Table of Contents
- Short Answer: Stock Parts by Failure Consequence and Verified Fit
- Build the Inventory From the Installed Machine Record
- Separate Wear Stock, Job Kits, and Downtime-Critical Spares
- Use the Operating Duty to Set a Reorder Decision
- Buy a Complete Changeout Scope, Not Only the Visible Wear Piece
- Protect Stored Parts From Mix-Ups, Damage, and Lost Traceability
- Put Parts Availability and Support in the Supply Scope
- Verify the Inventory Before Startup and After Each Changeout
- Common Buying Mistakes That Create a Spare-Parts Gap
- What to Send for a VSI Spare-Parts Proposal
- FAQ
- What spare parts should I keep for a VSI crusher?
- How many rotor tips should I stock?
- Can I use similar-looking VSI wear parts from another machine?
- Should I keep a complete spare rotor?
- What should a VSI changeout kit include?
- How should VSI crusher spare parts be stored?
- How can I check a supplier’s claimed parts availability?
- When should I reorder VSI wear parts?
VSI Crusher Spare Parts Inventory: What to Stock Before Startup
A VSI crusher spare-parts inventory should be built from the exact installed machine—not from a generic list of “VSI parts.” Before startup, identify the model, serial number, rotor build, feed arrangement, installed wear package, drawing revision, and the parts needed for a planned changeout or a downtime-critical failure. Then separate routinely consumed wear items from a job kit and a small set of insured critical spares. Confirm every line with a supplier part number, compatibility record, storage condition, delivery lead time, and safe replacement procedure. Send the raw material, feed size, output size, capacity, site photos, maintenance plan, and budget range when requesting a parts proposal.
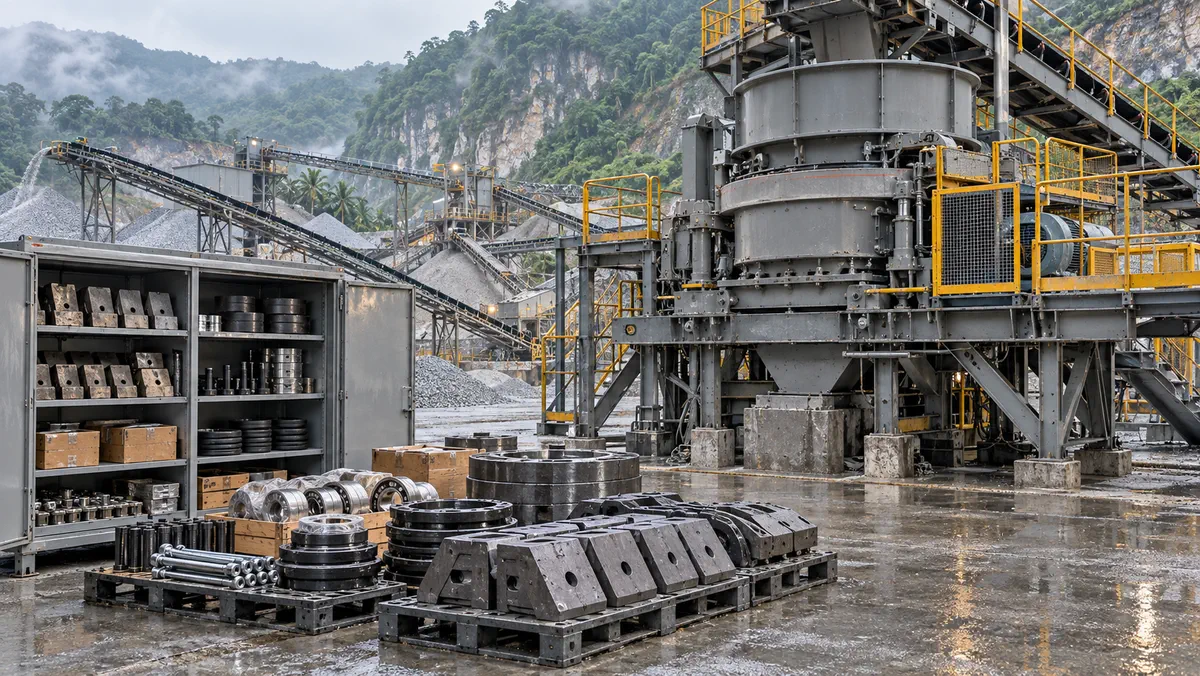
Short Answer: Stock Parts by Failure Consequence and Verified Fit
The right spare-parts list covers the items that are expected to wear under the planned duty, the components required for a defined maintenance job, and the few machine-specific parts whose absence could extend a stoppage beyond an acceptable window. It should not be a universal shopping list or a promise that one quantity suits every quarry.
Start with the installed-machine record. A part that appears similar can have a different rotor position, attachment detail, material grade, revision, or dimensional interface. Ask the OEM or authorized supplier to match the proposal to the serial number, rotor and chamber configuration, and current illustrated parts list before releasing an order.
Build the Inventory From the Installed Machine Record
The crusher nameplate is necessary, but it is rarely enough on its own. A useful inventory register links every stored item to the physical VSI it may serve and to the documents that show why it fits.
| Record to obtain | Why it controls the inventory | What to verify before ordering |
|---|---|---|
| Model and serial number | Identifies the actual production build rather than a family name | Photograph the nameplate and compare it with the supplier’s order acknowledgement |
| Rotor and chamber configuration | Changes the wear-package arrangement and the changeout scope | Rotor type, number and position of tips, backing pieces, anvils or rock-shelf components, and feed tube arrangement |
| Current illustrated parts list | Gives a controlled reference for part names and codes | Drawing or manual revision, current part number, any superseded part, and quantity per machine |
| Operating-duty record | Explains why a part is stocked and how urgently it may be needed | Raw material, abrasiveness, feed condition, hours, capacity, operating trend, and maintenance history |
| Maintenance-job plan | Stops a changeout from failing because a small associated item was omitted | Fasteners, retainers, seals, tools, lifting points, access, torque data, and inspection steps |
Treat the register as a handover document, not a spreadsheet that disappears after purchase. It should show where each item is stored, how it is preserved, which machine it fits, who can authorize its issue, and what document is consulted before it is installed.
This same identification discipline supports the broader VSI wear-parts review and helps prevent a rushed substitute part from being selected after an avoidable stoppage.
Separate Wear Stock, Job Kits, and Downtime-Critical Spares
Not every spare belongs in the same storage decision. Split the list into three groups so the site can decide what to consume, what to stage for a scheduled intervention, and what to insure against a long outage.
| Inventory group | Typical examples where fitted | Purchase decision | Do not assume |
|---|---|---|---|
| Operating wear stock | Rotor tips, backing pieces, anvils, liners, feed tube or distributor wear components | Hold a quantity based on verified consumption, planned inspection interval, supplier lead time, and storage capacity | That the same wear rate applies to a different rock, rotor speed, feed condition, or operating hours |
| Planned-changeout job kit | Complete approved set of wear components plus matching fasteners, retainers, seals, and specified consumables | Stage the exact scope for a scheduled shutdown and check it against the job plan | That loose headline parts alone will complete the work safely or restore the intended configuration |
| Downtime-critical spares | Machine-specific rotor or bearing-related assemblies, drive components, sensors, seals, or controls only where the supplier confirms them | Compare credible failure consequence and delivery risk with the cost and preservation burden | That every expensive component must be held locally, or that a warehouse item is interchangeable without records |
The priority is not simply “high price” or “high wear.” A low-cost fastener set may stop an otherwise complete rotor changeout. Conversely, a large assembly may be better covered by a documented supplier stock position, packing method, and transport plan than by years of unprotected site storage. Ask for the real decision inputs instead of defaulting to a fixed package.
Use the Operating Duty to Set a Reorder Decision
There is no responsible universal number of rotor tips, bearings, or assemblies to stock. The consumption and risk profile changes with material and operation. Define a reorder point only after the site has a baseline inspection record and the supplier has provided a verified lead-time statement.
| Decision input | How it changes the parts plan | Evidence to retain |
|---|---|---|
| Rock hardness and abrasiveness | Can alter wear pattern and the planned inspection or changeout frequency | Representative material description, test data if available, and inspection history |
| Moisture, clay, and feed preparation | Can affect material flow, buildup, access, and the reliability of wear observations | Feed photos, moisture or contamination observations, and the pre-screening arrangement |
| Rotor speed, cascade setting, and feed rate | Can change duty on wear components and the stability of operation | Approved settings, power trend, product sample record, and operator log |
| Capacity and shift pattern | Determines how quickly available stock is consumed before the next planned window | Run-hour record, tonnage estimate where available, and maintenance calendar |
| Supplier delivery path | Defines the risk if a needed part is not on site | Written quotation validity, lead-time basis, shipping route, packing, and destination terms |
Log the part code, installed date, inspected condition, removal reason, and operating condition for each changeout. The first few records may be incomplete, but they are more useful than copying another plant’s quantity. Link the decision to feed-rate control and wet-feed preparation, because an unstable feed can change both wear and the reliability of the operating record.
Buy a Complete Changeout Scope, Not Only the Visible Wear Piece
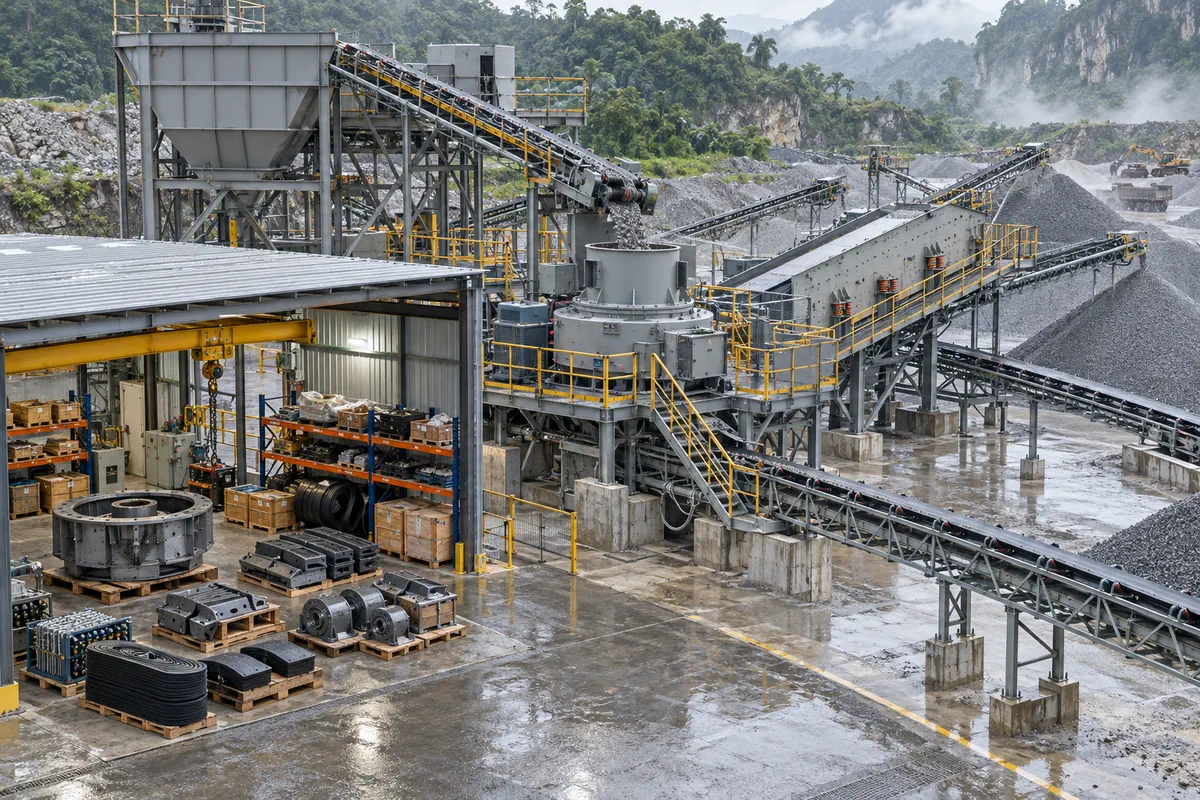
Before a shutdown, turn the planned job into a controlled kit. For each wear component or assembly, identify what else must be available to remove, inspect, install, secure, and return the machine to service under the approved procedure. The applicable OEM manual and site safety controls always govern the work.
- Confirm the exact part number, revision, quantity per machine, and position in the rotor or chamber.
- List all associated fasteners, pins, retainers, seals, gaskets, and specified consumables that are not safely reusable.
- Confirm approved lifting points, lifting-device interfaces, mass information, access constraints, and any special tools required for the selected work scope.
- Set the inspection and acceptance criteria for parts left in service, including what must be measured or photographed before a decision is made.
- Obtain the current installation instructions, torque or tightening method where applicable, guards, isolation requirements, and recommissioning checks.
Do not make an unsupported promise about torque values or a replacement interval in an RFQ. Request the controlled procedure for the installed model. A generic instruction found online can be older than the actual rotor build or omit the conditions that matter to the site’s lifting and guarding arrangement.
Protect Stored Parts From Mix-Ups, Damage, and Lost Traceability
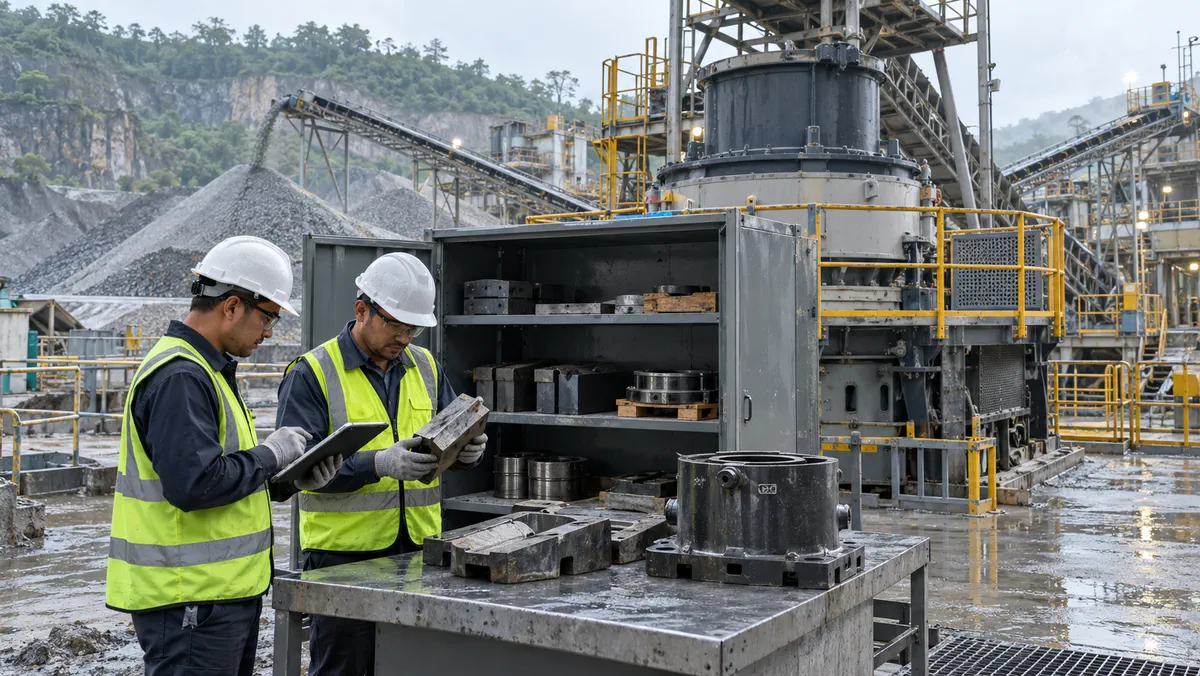
An unused spare only reduces downtime if it can be identified, found, and installed in acceptable condition. Store parts in the manufacturer’s packaging where practical, in a dry protected area, with the part code, revision, intended machine, received date, and preservation requirement recorded outside the package. Keep heavy components on rated supports with a safe retrieval method; do not create a storage arrangement that needs an unplanned lift or manual-handling workaround.
- Supplier part number, description, revision, and intended machine or rotor position.
- Quantity received, quantity issued, reserved quantity for a planned job, and physical storage location.
- Receiving inspection result, damage photos where relevant, packing condition, and any protective coating or shelf-life instruction.
- Linked purchase order, drawing or manual reference, supplier contact, verified lead-time date, and alternative-part approval status.
- Issue history and the reason a removed part was replaced, so the next order is tied to real condition rather than memory.
Avoid mixing used and new parts in one unmarked bin. Avoid removing labels before receiving inspection. Avoid declaring a part “available” if it is reserved for a scheduled job, damaged in storage, or not verified for the current machine revision.
Put Parts Availability and Support in the Supply Scope
The best time to resolve a parts question is before the plant needs the part. Ask the supplier for a proposal that makes both the scope and its limits visible.
- Which illustrated parts list and revision controlled the quotation?
- Which supplied parts are confirmed to fit the stated machine serial number and rotor or chamber build?
- What quantity is included per line, what is a full machine set, and which items are associated installation hardware rather than optional extras?
- What is the stated delivery lead-time basis, stock location at quotation date, packing method, shipment interface, and any export documentation requirement?
- Which items require special preservation, lifting equipment, tools, training, or a supplier technician?
- How are superseded part numbers, design changes, and urgent order identification handled?
- Which inspection records, manuals, installation instructions, and warranty terms are included?
This is also a buyer-protection issue when comparing supply routes. A lower quoted unit price may not represent the same revision control, included hardware, packing, or delivery risk. Use the same evidence-first comparison described in buying a mobile crusher from China rather than treating the word “spare” as a standard product.
Verify the Inventory Before Startup and After Each Changeout
Before commissioning, hold a short inventory verification with the site maintenance lead, commissioning representative, and parts supplier where practical. Compare physical items with the controlled list; do not wait for the first shutdown to discover an incorrect code or missing kit component.
- Match the crusher model, serial number, rotor build, and current drawings to the inventory register.
- Count each line, inspect packaging and storage condition, and photograph high-value or damage-sensitive items at receipt.
- Confirm that the planned first wear inspection has a complete job kit, approved procedure, safe access, isolation plan, lifting arrangement, and responsible person.
- Check the supplier contact path, order-reference process, delivery terms, and documented lead-time source for downtime-critical items.
- After a changeout, update the fitted parts, condition findings, quantity on hand, and reorder decision before the crew moves to the next urgent task.
Connect this record to the VSI commissioning checklist and to bearing-temperature checks. A parts list should support controlled inspection and troubleshooting, not encourage a parts swap before the feed, lubrication, operating trend, and safe procedure have been reviewed.
Common Buying Mistakes That Create a Spare-Parts Gap
- Ordering by crusher family name only. A model family can contain different rotor builds and revisions. Confirm serial-number compatibility and the current part reference.
- Buying only the visible wear component. A missing retainer, seal, fastener, tool, or approved lifting interface can delay a planned job.
- Copying a quantity from another quarry. Material, throughput, feed condition, duty hours, storage space, and delivery route change the right decision.
- Treating a quoted lead time as a permanent promise. Record its date, stock basis, shipping route, and conditions; check it again before reducing local inventory.
- Storing unmarked parts without preservation control. The item may become damaged, mixed with another revision, or impossible to issue confidently.
- Skipping the post-changeout record. Without fitted-date and condition information, the next purchase becomes another guess.
What to Send for a VSI Spare-Parts Proposal
Send the VSI model and serial number; photos of the nameplate, rotor, chamber, and current parts; the available illustrated parts list or manual revision; raw material and feed size; target output size; capacity and operating hours; wear and maintenance history; planned shutdown dates; site photos of storage and lifting access; destination and delivery preference; and budget range. If a part has failed or worn unexpectedly, include clear photos and the operating symptoms, but do not rely on a photo alone for part identification.
With that information, the supplier can separate a routine wear package from the first planned job kit and any downtime-critical spares, state the missing records, and make the proposal auditable before the plant is under pressure.
FAQ
What spare parts should I keep for a VSI crusher?
Keep parts according to the installed machine, operating duty, planned maintenance job, and delivery risk. A typical review may include rotor wear components, associated hardware, and a limited number of downtime-critical items, but the exact list must be matched to the serial number, rotor configuration, and supplier part records.
How many rotor tips should I stock?
There is no universal quantity. Set stock from the verified tips-per-rotor arrangement, the site’s inspection and wear history, planned shutdown interval, supplier lead time, and the number of complete changeout sets the site chooses to protect.
Can I use similar-looking VSI wear parts from another machine?
Do not assume so. Similar-looking parts can differ in position, dimensions, attachment method, material, or revision. Obtain written compatibility confirmation from the OEM or authorized supplier for the installed machine.
Should I keep a complete spare rotor?
A complete rotor or major assembly is a commercial risk decision, not a default requirement. Compare the verified repair or supply lead time, credible failure consequence, storage and preservation needs, lifting capability, and budget with a documented supplier support plan.
What should a VSI changeout kit include?
It should include the approved parts and all associated items required by the controlled job plan, such as specified fasteners, retainers, seals, tools, lifting interfaces, procedures, and inspection requirements. Confirm the exact scope with the machine supplier.
How should VSI crusher spare parts be stored?
Use protected, traceable storage that retains the part number, revision, intended machine, received condition, and preservation instructions. Keep heavy items on safe rated supports and avoid mixing used, new, or unverified parts.
How can I check a supplier’s claimed parts availability?
Ask for the stock-location and lead-time basis at the quotation date, delivery route, packing and export scope, order-reference process, and confirmation that the listed code fits the stated serial number and rotor configuration.
When should I reorder VSI wear parts?
Reorder when the verified stock on hand, reserved changeout kit, expected consumption, and current supplier lead time no longer cover the site’s approved maintenance plan. Update that decision after each inspection and changeout.