Table of Contents
- The Short Answer: Temperature Is a Trend, Not a Universal Limit
- What a Bearing-Temperature Reading Can—and Cannot—Tell You
- Establish a Reference Condition During Commissioning
- Lubrication and Monitoring Scope to Require in a VSI Package
- A Safe, Evidence-Based Response to a Rising Temperature Trend
- Common Causes That Need Different Remedies
- Lubrication condition or delivery issue
- Mechanical installation or alignment issue
- Process overload or unstable material duty
- Instrumentation or control problem
- What to Ask Before Buying a VSI Crusher
- Cost and Reliability Factors Often Missed
- Common Buyer Mistakes
- Setting an alarm from a generic internet number
- Treating the oil unit as an accessory
- Investigating only the bearing
- Skipping the commissioning baseline
- FAQ
- What bearing temperature is too high for a VSI crusher?
- Can low oil level cause high VSI bearing temperature?
- Should I stop a VSI crusher when a bearing-temperature alarm occurs?
- Does hot weather always explain a higher bearing temperature?
- What monitoring should be included with a VSI lubrication system?
- Can unstable feed raise VSI bearing temperature?
- How often should VSI lubrication oil be tested or changed?
- What information should I send to a supplier after a temperature alarm?
- Request a VSI Reliability Review
VSI Crusher Bearing Temperature: Lubrication Checks, Alarm Limits, and Failure Prevention
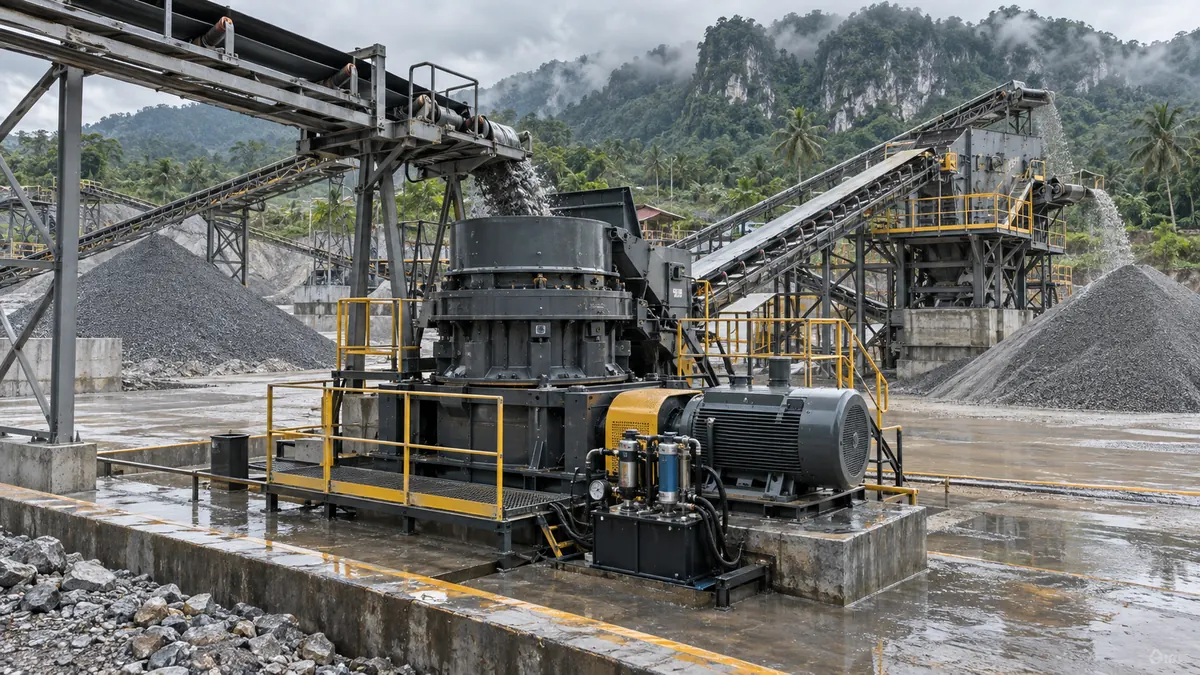
High bearing temperature on a VSI crusher is a warning to investigate, not a standalone diagnosis or a reason to copy a generic alarm setpoint. The correct response starts with the machine supplier’s approved limits for the bearing design, lubricant, sensor position, ambient condition, and operating duty. Then compare the present temperature trend with a stable baseline while checking oil level and condition, filter restriction, flow or pressure indication, cooler performance, drive alignment, vibration, feed stability, and the actual rotor duty. For buyers, the reliable choice is a VSI package with a defined lubrication and monitoring scope, clear alarm/trip philosophy, access for inspection, and commissioning records—not simply a crusher supplied with a motor and an unspecified oil unit.
The Short Answer: Temperature Is a Trend, Not a Universal Limit
Bearing temperature can rise because the bearing is overloaded, lubrication is unsuitable or restricted, oil is contaminated, cooling is inadequate, alignment or installation is wrong, a sensor is misleading, or the machine is operating outside its intended material and rotor duty. Several of these conditions can exist at once.
That is why a single temperature number from another brand, bearing arrangement, or sensor location should not be used as an operating rule. A sensor mounted on a housing will not necessarily read the same as a sensor near an oil return, and a normal trend at one ambient temperature may need different interpretation during a hot, dusty shift. Use the OEM’s approved warning and shutdown values for the supplied machine. Treat a sustained change from the commissioned baseline, a rapidly rising trend, or a temperature difference between comparable locations as a prompt for an orderly, safe inspection according to the supplier’s instructions.
Before interpreting a temperature change, make sure the operating condition is comparable. Feed size, moisture, rotor speed, feed rate, circulating load, product target, ambient temperature, and run time can all change the load seen by the machine. Our VSI feed-rate control guide explains why an unstable feed can make mechanical and process signals difficult to compare.
What a Bearing-Temperature Reading Can—and Cannot—Tell You
Temperature monitoring can reveal change before a failure becomes obvious. It is not a substitute for oil analysis, vibration checks, physical inspection, or the correct lockout and safety procedure.
| Observation | What it may indicate | What to verify before concluding |
|---|---|---|
| A gradual rise from the established baseline | Deteriorating lubrication, cooler performance, contamination, increasing load, or changing ambient conditions | Operating duty, oil level and condition, filter indication, cooler cleanliness, and trends from other sensors |
| A rapid increase | Restricted flow, a cooling problem, abnormal mechanical condition, wrong lubricant, sensor fault, or sudden duty change | Follow the OEM alarm/shutdown procedure; confirm signal, oil-circulation evidence, power trend, vibration, and safe access conditions |
| One side hotter than a comparable location | Uneven load, installation/alignment issue, unequal cooling or lubrication path, or different sensor placement | Sensor position, wiring, bearing arrangement, oil route, coupling/alignment history, and vibration data |
| Higher temperature only at high production rate | Rotor duty, feed changes, return load, power demand, or cooling capacity under sustained load | Material basis, feed stability, motor trend, screen/return load, ambient conditions, and commissioning record |
| No response when duty changes | Faulty sensor, wiring, display scaling, or unsuitable sensor location | Signal test, trend recording, panel configuration, and supplier-approved measurement point |
Do not open guards, touch rotating parts, bypass a trip, or change lubrication specifications based only on an alarm. The equipment manual and the site’s isolation procedure govern safe inspection and restart.
Establish a Reference Condition During Commissioning
The most useful temperature number is often the one recorded when the new or overhauled machine is operating steadily on a named material and product duty. Ask the supplier or commissioning team to document a reference condition rather than leaving a site with only alarm values.
- Bearing and sensor locations, sensor type, display tag, and whether the reading is housing, oil supply, or oil return temperature.
- Rock type, feed-size distribution, moisture/natural fines, rotor configuration, average feed rate, product target, and circulating-load condition.
- Ambient temperature, run time before readings, motor current or power trend, and relevant vibration readings.
- Approved lubricant type and grade, oil fill level, filter arrangement, cooler type, and observed flow/pressure indication.
- OEM-approved warning, shutdown, reset, and restart requirements for the supplied equipment—not generic settings.
This lets operators compare like with like. If a VSI changes from dry crushed rock to wetter feed with more fines, its load and cooling conditions may differ even when the displayed tonnes per hour look similar. See VSI wet-feed pre-screening and washing decisions before assuming that a material change affects only throughput.
Lubrication and Monitoring Scope to Require in a VSI Package
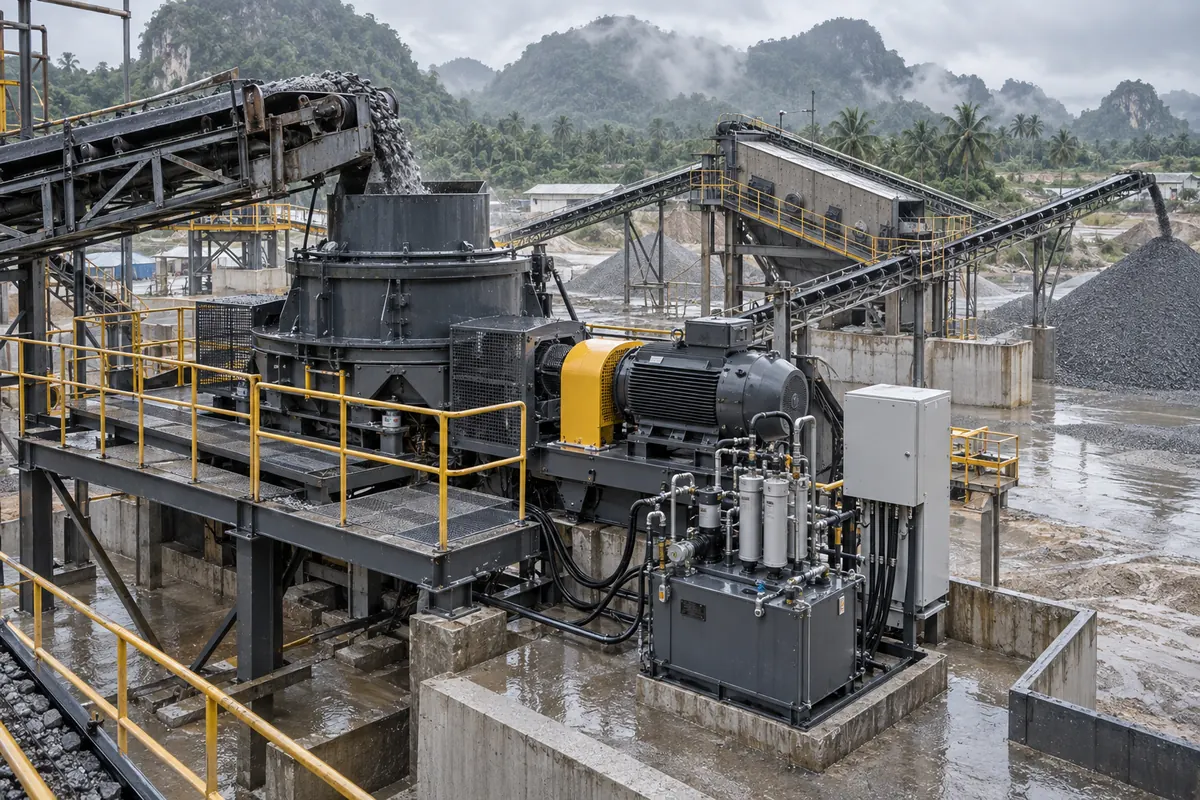
| Scope item | Why it matters | Buyer question to put in the proposal |
|---|---|---|
| Lubricant specification | The wrong oil type or grade can affect film strength, flow, temperature behavior, and warranty requirements | Which lubricant is approved for this bearing and climate, and who supplies the initial fill? |
| Reservoir, pump, and filtration | Oil storage, circulation, and filtration must suit the duty and contamination risk | What are the reservoir capacity, pump duty, filter rating, service interval, and restricted-filter indication? |
| Cooling arrangement | Cooling capacity and maintenance access affect steady-state temperature | Is cooling air or water based; what ambient/load assumptions are stated; and how is the cooler cleaned safely? |
| Temperature, pressure, and flow monitoring | An alarm is useful only when the measurement point and action are understood | Which signals go to the PLC, and which events generate alarm, interlock, or shutdown? |
| Hoses, fittings, and cable routing | Vibration, abrasion, heat, and poor routing can create leaks or signal faults | Are hoses and cables protected, shown in drawings, and accessible without removing major guards? |
| Commissioning and spares | The plant needs a supportable baseline and achievable maintenance plan | What trend data, spares, drawings, manuals, and remote-support scope are included? |
The supplier should state whether the lubrication unit is factory-mounted, skid-mounted, or installed separately; which items ship loose; and which field piping, wiring, controls integration, foundations, and guarding remain in the buyer’s or EPC contractor’s scope.
A Safe, Evidence-Based Response to a Rising Temperature Trend
Use the machine maker’s operating manual and site safety procedure first. This sequence organizes evidence and supplier communication; it does not replace equipment-specific shutdown or maintenance instructions.
- Confirm the alarm context: record time, run hours, sensor tag, displayed value, alarm state, product duty, feed condition, power trend, and ambient condition.
- Follow the approved protective action: respect the programmed warning, trip, cooldown, isolation, and restart conditions; never defeat a protective device to maintain production.
- Check process changes: compare feed size, moisture, feeder stability, rotor setting, screen load, return load, and production target with the reference condition.
- Inspect lubrication evidence safely: under the correct isolation and access controls, check specified oil level, leaks, cooler condition, filter indication, hoses, connectors, and permitted monitoring points.
- Confirm data quality: check sensor identity, wiring, controller display, and whether another approved measurement supports the indication.
- Escalate with complete information: send logged data, photos, oil-test and vibration data if available, maintenance history, and material/process changes.
In a closed circuit, track return load independently. A screen or return-conveyor restriction can change the crusher’s real duty even when fresh-feed measurement is steady. Read our closed-circuit versus open-circuit VSI guide for the relevant measurement boundaries.
Common Causes That Need Different Remedies
Lubrication condition or delivery issue
Oil degradation, contamination, incorrect fill level, restricted filtration, damaged hoses, unsuitable lubricant, or poor cooler performance can each affect temperature. Establish the approved oil, laboratory result, circulation evidence, and maintenance history before selecting a remedy.
Mechanical installation or alignment issue
Bearing fit, drive alignment, coupling condition, base stiffness, fastener integrity, and an earlier repair can affect the load path. Temperature trends alongside vibration and maintenance history help the OEM decide whether a mechanical inspection is required.
Process overload or unstable material duty
Oversize feed, feed surges, high circulating load, more abrasive rock, wet fines, or a rotor duty different from the quotation basis can increase mechanical duty. Stabilize the process before assuming the problem belongs only to the bearing. Our VSI feed-size control guide helps define the upstream boundary.
Instrumentation or control problem
A damaged probe, loose connection, incorrect scaling, or mismatched sensor location can produce a misleading reading. Instrument checks should be systematic and documented; changing a threshold without proving the sensor and condition can hide a real problem.
What to Ask Before Buying a VSI Crusher
- Bearing arrangement and OEM-approved lubricant specification for the proposed configuration and expected climate.
- Sensor locations, variables monitored, PLC/remote-monitoring interface points, and alarm/trip philosophy.
- Cooler, pump, filters, hose/cable protection, maintenance access, and required utilities.
- Commissioning procedure, baseline data to hand over, training scope, and any controls-integration exclusions.
- Consumables, critical spares, service tools, recommended oil-testing approach, and normal lead times.
- Material basis for capacity and rotor duty: raw material, feed size, output size, capacity, moisture/fines, power supply, and operating hours.
This makes quotations comparable. One supplier may offer only a crusher skid, while another includes the instrumentation, oil unit, commissioning records, and support needed to operate predictably. For a commercial comparison method, see how to compare VSI power consumption per tonne and select a motor.
Cost and Reliability Factors Often Missed
The lowest equipment price can exclude work essential to reliable operation: filtered and cooled oil circulation, protected sensor routing, sensible controls, commissioning time, lubricant and filter spares, access platforms, oil-sampling points, and evidence-based training. Also consider the cost of downtime if filters, seals, sensors, hoses, bearings, or specialized support are not locally available.
Do not compare warranty statements without reading their operating and maintenance conditions. The buyer should know who records baseline data, who approves the lubricant, what records are needed for support, and whether material or throughput changes require a revised duty review.
Common Buyer Mistakes
Setting an alarm from a generic internet number
Alarm and shutdown values depend on the actual bearing, lubricant, sensor location, and OEM design. Ask for the values and action logic for the offered configuration rather than copying a figure from another machine.
Treating the oil unit as an accessory
The oil system, cooler, filters, sensors, controls, and access points are part of the crusher’s reliability scope. Review them as carefully as the rotor and motor.
Investigating only the bearing
A process overload, wet material, return-load increase, alignment issue, or sensor fault can all change the reading. Log the full operating condition before deciding on the cause.
Skipping the commissioning baseline
Without a named reference condition, the site has no reliable way to identify a meaningful trend. Include handover data in the commissioning deliverables.
FAQ
What bearing temperature is too high for a VSI crusher?
Use the equipment supplier’s approved warning and shutdown limits for the exact bearing, lubricant, sensor position, and machine configuration. A sustained departure from the commissioned baseline or a rapid rise also needs investigation, even if it has not reached a copied generic number.
Can low oil level cause high VSI bearing temperature?
It can contribute, but it is only one possible cause. Confirm the approved level, oil condition, circulation, filter restriction, cooling, operating load, and sensor validity using the supplier’s procedure.
Should I stop a VSI crusher when a bearing-temperature alarm occurs?
Follow the OEM alarm, trip, cooldown, isolation, and restart instructions installed for the machine. Do not bypass alarms or continue operation against the supplied protective logic to keep production running.
Does hot weather always explain a higher bearing temperature?
Ambient temperature can influence cooling performance, but it should not dismiss a trend. Compare it with the commissioning baseline, duty, oil condition, cooler performance, and the supplier’s stated environmental assumptions.
What monitoring should be included with a VSI lubrication system?
Request the measurement points, sensor locations, alarm/trip logic, oil circulation and filtration details, cooling arrangement, PLC interface, and commissioning records in writing.
Can unstable feed raise VSI bearing temperature?
Unstable feed can change rotor duty, power, and internal recirculation, which may affect the operating condition. Check feed size, moisture, feeder stability, screen performance, and return load alongside lubrication and mechanical data.
How often should VSI lubrication oil be tested or changed?
Use the machine supplier’s lubricant and maintenance schedule, adjusted only through an evidence-based site plan. Oil condition, contamination risk, operating hours, ambient conditions, and laboratory results are more useful than an arbitrary calendar interval.
What information should I send to a supplier after a temperature alarm?
Send the sensor reading and trend, alarm time, run hours, material and feed condition, throughput, power/current trend, ambient condition, oil details, maintenance history, site photos, and relevant control screenshots.
Request a VSI Reliability Review
Send MVSI your raw material details, normal and maximum feed size, moisture and fines observations, required output size, target capacity, current VSI model and rotor information, temperature/power/vibration trends if available, lubrication-system photos, site photos, available power, operating hours, and budget range. We can help define the information needed to evaluate the feeder, rotor duty, drive, lubrication, monitoring, screen, and support scope. Final selection and operating limits must be confirmed against the supplied machine documentation, representative material, and the agreed commissioning method.