Table of Contents
- Information Gain: Separate Factory Evidence From Site Performance
- Agree the FAT Scope Before Anyone Travels
- Verify the Ordered Machine and Visible Build
- Witness Functional Checks Only Against an Agreed Method
- Review Documents, Interfaces, and Open Items Before Release
- Check Packing, Preservation, and Shipment Readiness
- Buyer Checklist for a VSI Crusher FAT
- Send MVSI Crusher the Acceptance Basis Before Shipment
- FAQ
- What is a factory acceptance test for a VSI crusher?
- Can a VSI FAT prove the crusher capacity?
- What documents should be reviewed during a pre-shipment inspection?
- Should buyers check the VSI serial number before shipment?
- Is a no-load rotation test enough for final acceptance?
- What should go in a factory acceptance exception list?
- Should spare parts be checked at the FAT?
- What information should I send before arranging a VSI factory inspection?
Before a VSI crusher leaves the factory, buyers should confirm that the delivered machine, documented scope, interfaces, safety items, and shipment pack match the approved order—not simply watch it turn. A useful factory acceptance test (FAT) combines identification and dimensional checks, visible mechanical inspection, guard and access review, agreed functional checks where safely practical, documentation review, and a signed exception list. It cannot prove site throughput, sand grading, wear life, or plant performance on its own; those depend on the actual material, circuit, installation, and operating conditions. The acceptance record should state what was witnessed, what remains site-dependent, and who closes every open item before release.
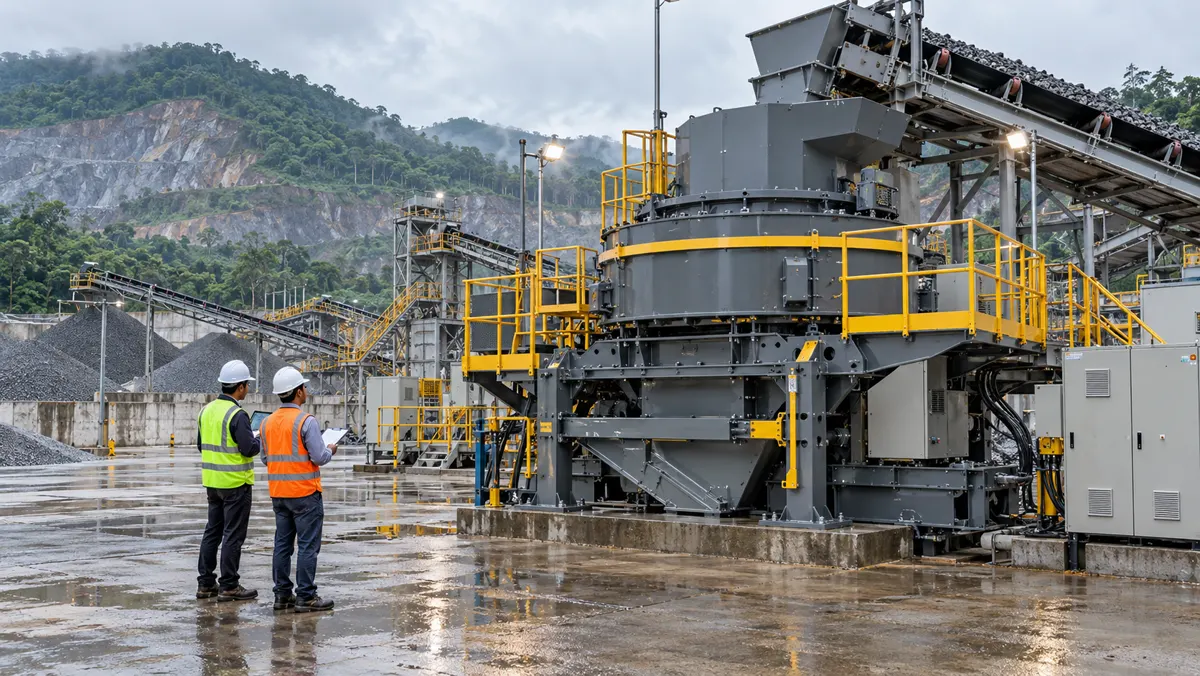
Information Gain: Separate Factory Evidence From Site Performance
Many pre-shipment checklists stop at paint, packaging, and a nameplate. That is not enough for a buyer who must integrate a VSI into a real crushing circuit. The useful acceptance boundary is to confirm the order-specific machine, interfaces, visible build, supplied scope, records, and unresolved actions before release—then identify which outcomes can only be checked after installation with the intended material.
Do not turn a short factory run into an unsupported capacity or product-quality guarantee. The VSI crusher commissioning checklist explains why final acceptance needs controlled feed, product sampling, electrical trends, safeguards, and records at the installed plant.
Agree the FAT Scope Before Anyone Travels
An acceptance visit is most useful when the buyer and supplier agree the witness points before the machine is prepared for dispatch. The purchase order, approved layout, equipment list, interface schedule, and inspection procedure should use the same revision basis. If a third-party inspector or EPC team is involved, give each party the checklist and evidence format in advance.
| FAT scope item | What to agree before the inspection | Buyer risk if it is left vague |
|---|---|---|
| Machine identity | Model, serial number, approved configuration, drawing revision, and order reference | A similar-looking unit or an unapproved component can be accepted by mistake |
| Supply boundary | What is included for the crusher, drive, guards, platforms, controls, tools, spares, and loose items | Gaps may only appear during installation or startup |
| Witness points | Which checks require the buyer, inspector, supplier representative, or photographs | A late visitor may have no evidence of an important check |
| Functional method | Whether a no-load or limited functional check is possible, safe, and included in the contract | An informal demonstration can be misread as a performance test |
| Acceptance records | Checksheet, photographs, certificates, packing list, and non-conformance log | Open items can disappear into email without an owner or due date |
Ask for the exact identification method used on the selected equipment. A model designation alone may not distinguish rotor build, drive arrangement, electrical standard, liner or wear-part selection, service access, or options agreed after the first quotation. The VSI spare-parts inventory guide is relevant because the final parts list should also match the confirmed machine and rotor configuration.
Verify the Ordered Machine and Visible Build
The first physical check is not a general walk-around. Compare the visible machine and its supplied items with the current approved documents. Photograph the identification plate or agreed serial-number location, but keep confidential records within the project team where needed.
| Inspection area | What a buyer can verify at the factory | What still needs later validation |
|---|---|---|
| Crusher and rotor assembly | Agreed model/build, accessible covers, visible fasteners, guards, liners or wear arrangement where inspection is permitted | Performance on the actual feed, wear life, and final operating setting |
| Drive and motor base | Agreed motor/drive scope, mounting, guarding, cable-entry boundary, and accessible service points | Alignment after transport and installation, electrical behavior under process load |
| Feed and discharge interfaces | Flange, hopper, chute, skid, or conveyor interfaces against approved dimensions and responsibility schedule | Match to final site steelwork, elevations, trajectories, and material flow |
| Access and guarding | Platforms, handrails, guard panels, inspection doors, lifting provisions, labels required by contract | Site-wide traffic, lockout, emergency response, and operating procedures |
| Loose items and spares | Agreed tools, fasteners, sensors, manuals, and packaged spare scope against the packing list | Quantity and replenishment plan for the actual maintenance program |
Check that inspection covers and guards can be opened only using the documented safe method and that the required access space is realistic. A guard that fits at the factory can still conflict with a site platform, chute, cable route, or lifting beam. Use the foundation and installation civil-work checklist to review the interfaces that must be confirmed before civil release.
Witness Functional Checks Only Against an Agreed Method
A factory functional check can be valuable when it follows an agreed and safe method. Its purpose may be to confirm a defined rotation direction, motor/control interface, basic indication, or another contract-specified point. The manufacturer should control the method, isolation, guarding, and permitted access. Do not improvise a test from a buyer checklist.
The record should say what was demonstrated, for how long, under what condition, and what was not tested. For example, an unloaded rotation check does not demonstrate the final material duty. It does not prove product grading, feed acceptance, capacity, power per tonne, vibration behavior on site, or the performance of the full screen and return circuit.
The VSI power-consumption guide explains why energy evidence needs a defined material-and-circuit basis. Likewise, the feed-rate control guide shows why stable plant feed cannot be inferred from a factory observation alone.
Review Documents, Interfaces, and Open Items Before Release
The document review is where a buyer turns a visual inspection into a controlled handover. Request the current approved version of the documents that define the delivered scope, then compare their references with the machine, loose items, packing list, and acceptance record.
At a minimum, ask the supplier which documents are included with the order and which are still preliminary. Depending on the scope, that may include general-arrangement drawings, foundation/load information, electrical interface data, operation and maintenance manuals, parts information, packing list, test or inspection records, and preservation or storage instructions. Treat every document as model- and project-specific until confirmed by the issuing supplier.
For every deviation, use a short exception log:
- Describe the observation precisely, including the drawing or order reference.
- Mark whether it blocks dispatch, can be closed before dispatch, or is a controlled site action.
- Assign one responsible party, evidence required for closure, and a target date.
- Record whether the buyer accepts a concession, requests rework, or needs an engineering clarification.
- Keep the final closure evidence with the factory acceptance record and shipment documents.
This protects both sides. A list of verbal promises is difficult to audit after containers, steelwork, and site labor have been booked.
Check Packing, Preservation, and Shipment Readiness
Pre-shipment inspection also covers what happens between the factory floor and the installation site. Confirm that loose components are identified, vulnerable surfaces are protected as specified, and the packing list lets the receiving team reconcile every package. Export packing, lifting points, container loading, climate protection, storage duration, and customs documentation are project-dependent; agree the expected standard before the visit instead of assuming a generic crate is suitable.
The buyer should also identify what must travel separately: special tools, spare wear parts, manuals, electrical items, cables, sensors, bolts, and small loose hardware can be easy to miss after the main crusher body arrives. Where an item is packed inside a crate or attached to a skid, make the location visible on the packing record.
Buyer Checklist for a VSI Crusher FAT
- Bring the latest purchase order, approved equipment list, relevant drawings, scope matrix, and agreed inspection checklist.
- Confirm the machine identity, serial-number record, ordered configuration, major interfaces, and visible access/guarding against the approved documents.
- Reconcile crusher, drive, platform, controls, loose items, tools, and spares against the agreed supply boundary.
- Witness only the functional checks that are safely available and contractually agreed; record conditions, results, and untested items.
- Review current operation, maintenance, interface, packing, and preservation documents with their revision references.
- Photograph agreed evidence points and record every deviation in an owned exception log with closure evidence and due date.
- Check package identification, loose-item locations, protection, packing list, lifting/receiving information, and storage requirements.
- Reserve final material-duty, product, electrical-load, and plant-safety acceptance for the installed commissioning plan.
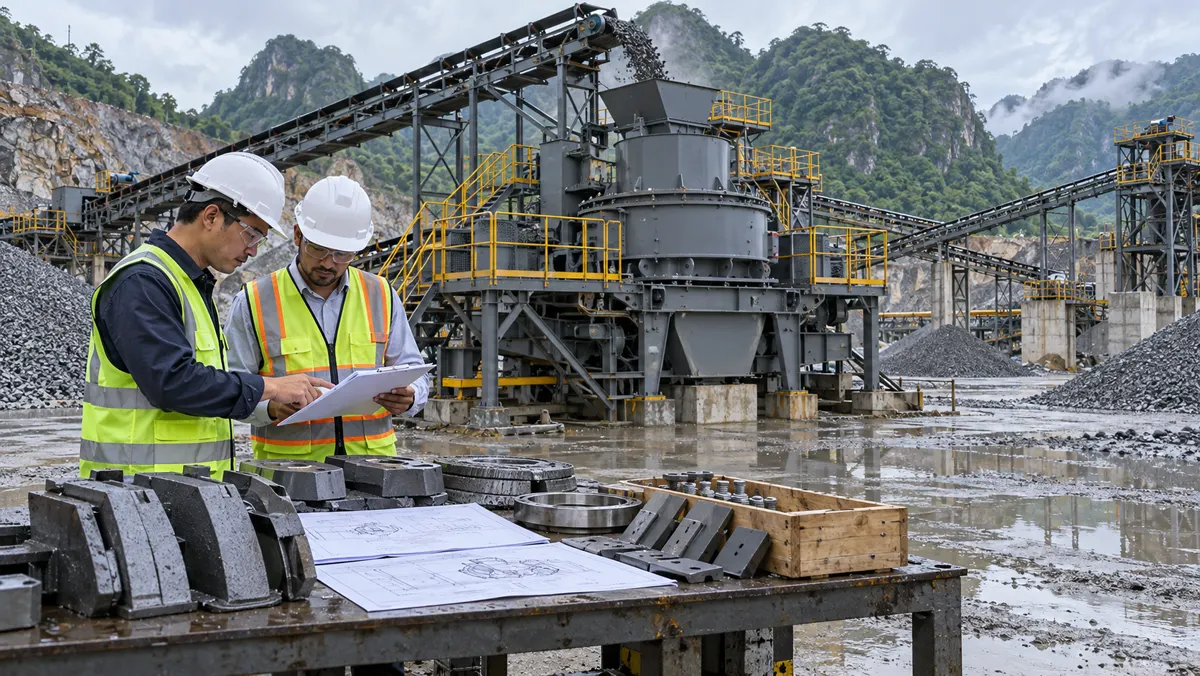
Send MVSI Crusher the Acceptance Basis Before Shipment
For an order-specific pre-shipment inspection discussion, send MVSI Crusher your raw material, feed size, output requirements, target capacity, approved equipment scope, current drawings, site photos, installation interfaces, and budget range. We can help identify which machine and documentation checks belong in the factory acceptance record, which items need a site verification plan, and which assumptions must be confirmed before release.
FAQ
What is a factory acceptance test for a VSI crusher?
It is an agreed pre-shipment inspection and record process used to confirm the ordered equipment, supplied scope, visible build, interfaces, documents, packaging, and open items. The actual witness points depend on the purchase order, approved documents, safety method, and supplier procedure.
Can a VSI FAT prove the crusher capacity?
Usually no. A factory check does not reproduce the actual material, feed gradation, moisture, screening, recirculation, installation, and operating settings. Treat capacity and product outcomes as site-dependent unless a separate, agreed test establishes a defined basis.
What documents should be reviewed during a pre-shipment inspection?
Review the current approved order scope, equipment list, layout or interface drawings, operation and maintenance information, parts list, packing list, inspection record, and any project-specific electrical, foundation, preservation, or shipping documents that are included in the contract.
Should buyers check the VSI serial number before shipment?
Yes. Record the agreed identification information and connect it to the approved configuration, order reference, documents, loose items, and acceptance record. Follow the supplier’s documented identification method and project confidentiality rules.
Is a no-load rotation test enough for final acceptance?
No. It may confirm only the limited points defined in the agreed safe test method. It does not replace site commissioning with the intended material, circuit, guarding, controls, product sampling, and operating records.
What should go in a factory acceptance exception list?
Each entry should state the observation, relevant order or drawing reference, dispatch impact, owner, closure evidence, target date, and the buyer’s decision to accept, request rework, or seek clarification.
Should spare parts be checked at the FAT?
Yes, when they are part of the purchase scope. Reconcile their part references, quantity, packaging, and location with the confirmed machine configuration and packing list; do not assume a generic spare list fits every VSI build.
What information should I send before arranging a VSI factory inspection?
Send the purchase order scope, equipment list, approved drawings, current inspection points, required documents, shipping constraints, site photos, raw material, feed size, output, capacity, interface information, and budget range so the inspection boundary can be coordinated clearly.